As global cooling demand rises, manufacturers face tighter expectations for speed, accuracy, and energy efficiency. The International Energy Agency’s The Future of Cooling reports that space-cooling electricity demand could more than triple by 2050. Its projection reaches approximately 6,200 TWh annually. The 2023 UNEP Global Cooling Watch report also highlights rapid cooling growth in emerging markets. These pressures reach the production line. An Aluminum Fin Press Machine must form consistent fins without damaging thin aluminum sheets.
Supplier selection therefore requires more than a catalog review. Buyers should examine press capacity, stroke stability, fin height control, tooling compatibility, and verified production references. Cycle speed matters. So does repeatability. A machine running at 120 strokes per minute may appear attractive, yet unstable feeding can create costly scrap. The real test is sustained performance across different aluminum gauges.
Reliable suppliers usually provide documented tolerances, factory acceptance testing, maintenance schedules, and responsive technical support. ISO 9001 certification can support process confidence, but it does not replace an on-site audit or sample trial. That distinction matters. Supplier rankings can simplify research, but no universal list fits every factory. A compact HVAC workshop needs different automation than a high-volume automotive heat-exchanger plant.
This guide compares leading Aluminum Fin Press Machine suppliers worldwide through practical and technical criteria. It considers engineering experience, tooling expertise, delivery capability, after-sales service, and customer evidence. Some published specifications remain difficult to verify. Buyers should question them. A careful decision combines reports, factory observations, test results, and realistic production requirements.
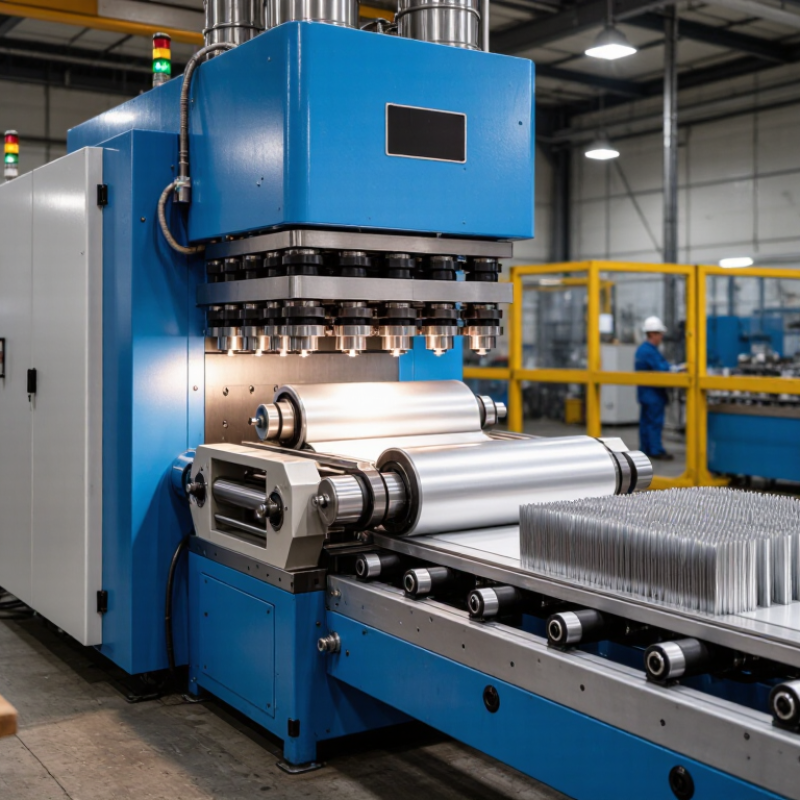
Aluminum fin press machines transform narrow aluminum strip into cooling fins for heat exchangers, radiators, and air-conditioning systems. Strip thickness commonly ranges from 0.05 to 1.5 mm. A 0.05 mm strip behaves like foil, while 1.5 mm material needs far greater forming force. That range is not a marketing detail. It affects die clearance, feed stability, burr control, and press capacity. The International Aluminium Institute reported approximately 70 million tonnes of primary aluminum production in 2023, showing the scale behind this manufacturing chain.
A capable fin press usually combines decoiling, straightening, servo feeding, piercing, louvering, forming, cutting, and stacking. Some lines also control fin pitch automatically. Suppliers should disclose stroke rate, working width, maximum strip strength, and repeatability data. A fast machine is not always the best machine. Poor feeding can create uneven louvers within one coil. That defect may remain invisible until airflow testing.
For worldwide sourcing, buyers should inspect trial-run records and tooling wear data. Aluminum foil near 0.05 mm needs gentle tension control and highly polished guides. Thicker strip demands stronger frames and reliable overload protection. The U.S. Department of Energy identifies heat exchangers as important efficiency components in cooling systems, which reinforces the value of consistent fin geometry. In practice, setup time can still disappoint, especially when operators change materials frequently. A supplier’s training support, spare-tool availability, and documented maintenance intervals deserve the same attention as headline speed.
Global Supplier Regions: China, Germany, Italy, Japan, and the United States
China offers a broad supplier base for aluminum fin press machines, from standard production lines to customized systems. Buyers often find competitive pricing and flexible engineering support. Factory visits can reveal practical details, including press rigidity, feeder alignment, and spare-part storage. Documentation quality varies, so technical drawings deserve careful review. Fast quotations are helpful, but they do not prove long-term reliability.
Germany is often associated with precise mechanical construction, detailed controls, and disciplined quality procedures. These machines may suit manufacturers with demanding tolerances and stable production plans.
Italy brings strong experience in forming equipment and integrated line design. Its suppliers commonly focus on compact layouts and operator-friendly setups. Some configurations can become complex, however. Maintenance teams should inspect access around dies, sensors, and lubrication points.
Japan is known for careful manufacturing practices, consistent motion control, and process stability. Japanese equipment may appeal to plants requiring repeatable fin geometry over long runs.
The United States provides suppliers with practical automation knowledge, service networks, and application-focused engineering. Local support can reduce downtime when training or troubleshooting is urgent.
Still, regional strengths are not guarantees. A supplier’s test records, material trials, safety documentation, and after-sales response matter more than origin alone. I would request sample fins from your actual aluminum coil, because catalog performance may not match the factory floor.
Selecting an aluminum fin press machine requires more than comparing supplier catalogs.
The International Aluminium Institute reported global primary aluminum production above 70 million tonnes in 2023. That scale increases demand for stable, high-volume fin forming. However, capacity must match the part, not the headline.
For compact heat-exchanger fins, a 10–100 ton press may handle thin strip and modest draw depth. Larger assemblies can require 200–500 tons, especially with thicker aluminum or multiple stations.
Speed also matters. A range of 50–600 strokes per minute covers development work through high-volume production. Yet 600 SPM can be misleading. Feed length, coil straightness, die design, and lubrication often limit real output.
The International Energy Agency continues to identify industrial efficiency as a major manufacturing priority, so unnecessary speed can increase energy use and scrap.
Fin accuracy should be verified at the required pitch, height, width, and burr level.
Use optical measurement, sample runs, and capability studies such as Cpk. A practical target may be ±0.02–0.05 mm for critical fin dimensions, but the drawing must decide. ISO 2768 can guide general tolerances, though it cannot replace product-specific requirements.
Supplier comparisons should include measured samples, repeatability data, noise levels, and maintenance records.
A common mistake is accepting the first trial result. It may be excellent, but inconsistent after several hours. A longer production test is wiser.
Top Aluminum Fin Press Machine Suppliers Worldwide
Supplier Evaluation: ISO 9001, ±0.02 mm Tolerance, and Tooling Life
Choosing an aluminum fin press supplier requires more than comparing machine prices. ISO 9001 certification should cover design, manufacturing, inspection, and corrective actions. Ask for the certificate scope and recent audit records. A certificate alone proves little.
The ±0.02 mm tolerance also needs careful verification. Request a stamped sample, dimensional report, and the measurement method used. Check whether the tolerance applies to fin height, pitch, width, or tooling alignment. These details matter. A supplier claiming universal precision may be overstating performance. Confirm calibration records for gauges, sensors, and inspection equipment. Ideally, review repeatability data from several production runs, not one polished sample.
Tooling life reveals practical engineering quality. Ask for expected cycles under your aluminum grade, thickness, speed, and lubrication conditions. Reliable suppliers should explain die steel, heat treatment, clearance settings, and maintenance intervals. They should also provide replacement-part drawings and service guidance. In real production, tooling life can fall sharply when operators adjust feed pressure without control. That risk is often overlooked. A trial run can expose burr formation, inconsistent fin spacing, or rising press load. Do not accept vague promises. Require measurable acceptance criteria, documented test results, and a clear response process when output misses tolerance. The best evaluation may still contain uncertainty, because material batches and operator habits change. That is worth recording.
Top Aluminum Fin Press Machine Suppliers Worldwide
Comparing aluminum fin press machines requires more than checking the purchase price. Ask suppliers for measured energy use per production cycle, not broad efficiency claims. A machine using 18 kWh per hour may cost more than expected during continuous operation. Check heater demand, servo consumption, compressed-air requirements, and standby usage. Small differences matter.
Lead time should include engineering, tooling, factory testing, shipping, installation, and operator training. Request a dated production schedule with clear milestones. A quoted eight-week delivery can become twelve weeks when custom dies are involved. Warranty terms also need careful reading. Confirm coverage for the main drive, control system, electrical components, and forming tools. Ask who pays for replacement parts, labor, and transport. Exclusions can be costly.
Total cost should include commissioning, spare parts, software support, maintenance, energy, and downtime. Compare at least three written quotations using the same fin dimensions and output target. A lower-priced machine may require more manual adjustments or frequent die replacement. I have seen buyers underestimate installation costs because factory power and floor preparation were ignored. My own early estimates were too optimistic. That mistake changed how I review supplier proposals. Request a sample run, inspect fin accuracy, and record cycle time before signing. Keep every assumption in writing.
If for some reason you did not find the service or product you need, you can always leave a request for a free consultation and get an answer.